
Vol. ZH · MFG · MMXXVI
Manufacturing field notes

SDS Drill Bit Manufacturing, Built in Full View.

Machining · Heat Treatment · Brazing · Straightening

Seven direct factory-floor records plus Zhonghuan's isothermal salt-bath and controlled-atmosphere heat-treatment routes connect body machining, heat treatment, carbide joining and straightening.

Enter the process archive
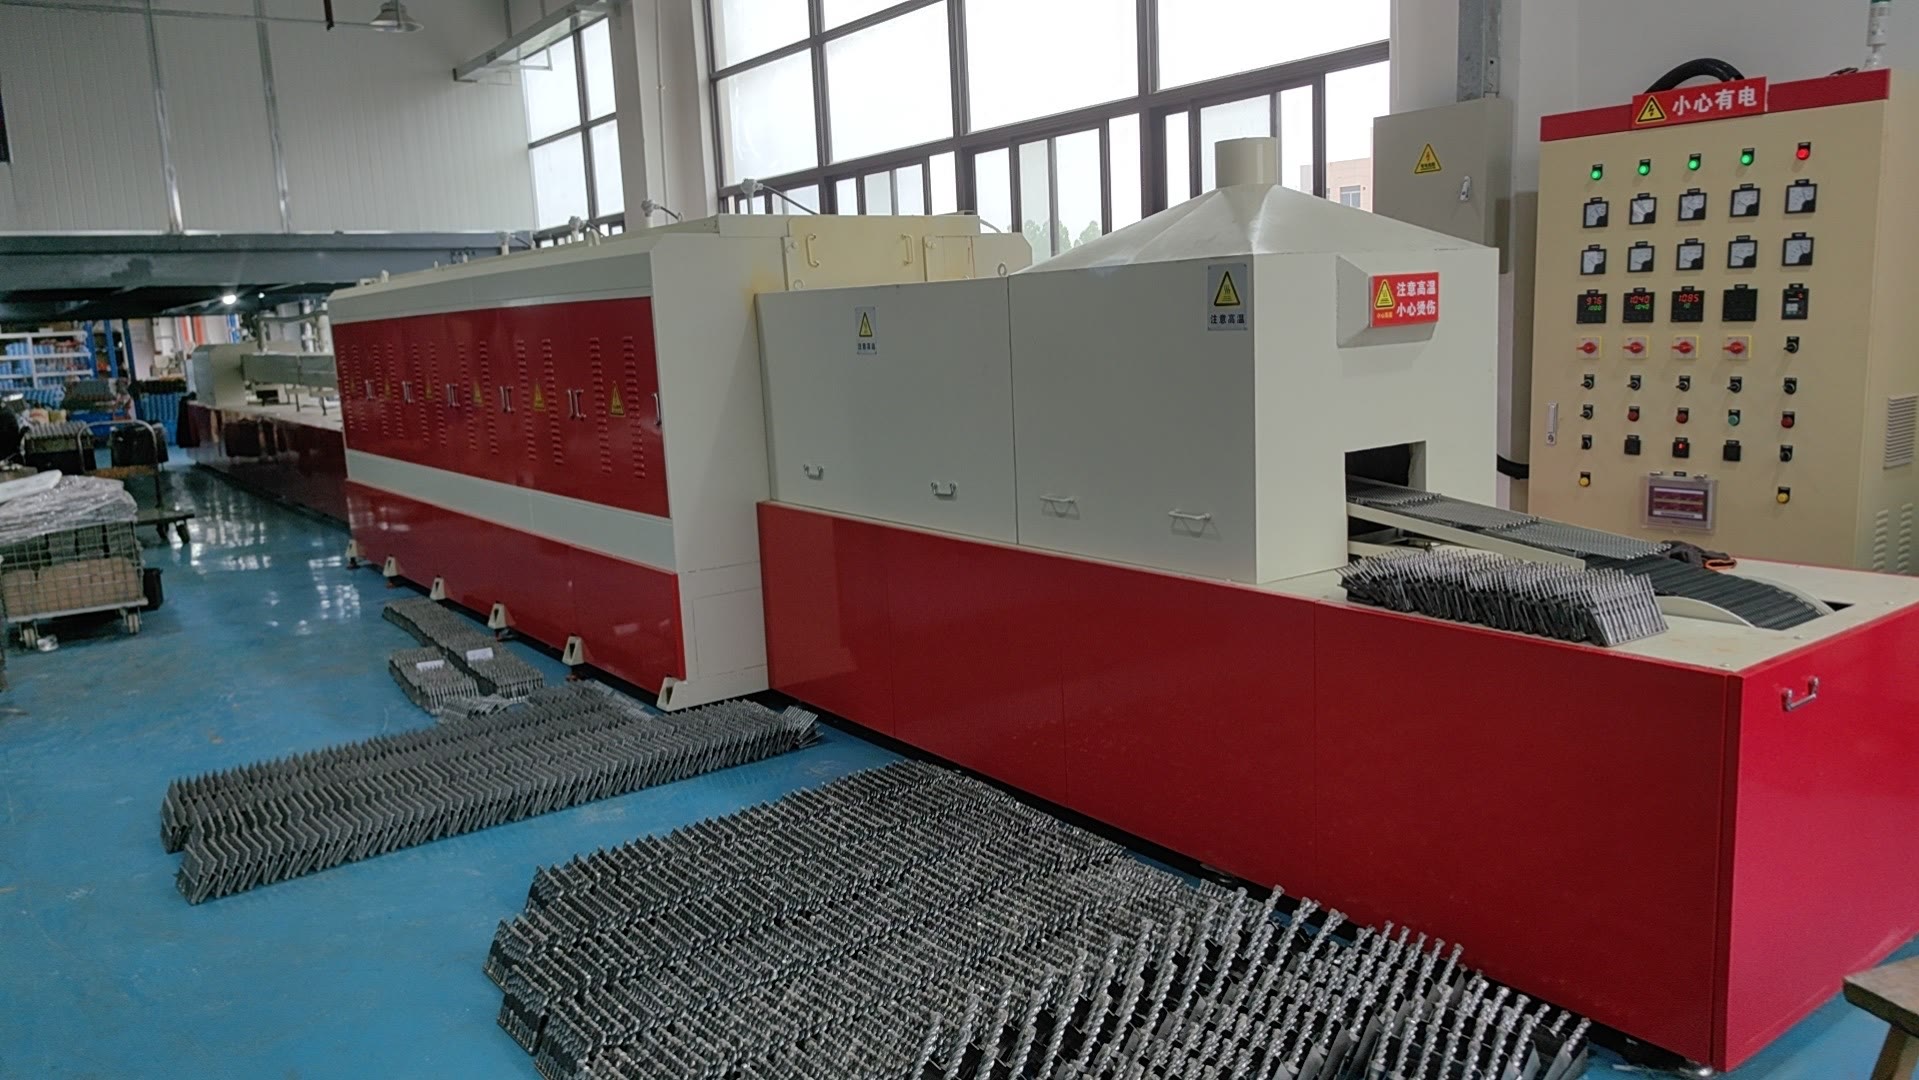
Continuous Controlled-Atmosphere Mesh-Belt Brazing Furnace
Still · 06 / 07
Continuous Controlled-Atmosphere Mesh-Belt Brazing Furnace Zhonghuan · Factory Floor
§ I · Machining 04 / 07 Records

Machining the Body and Shank.

Four records follow material removal at the spiral flute and connection end. The camera stays on the actual cutting cycle: feed, clamp, index, machine and unload.

Film · 01 · 0:36

Automated SDS-Plus Shank-Groove Machining

An automated station feeds finished drill bodies, clamps the shank and machines the SDS-Plus connection grooves.

Visible record — Automatic feeding, clamping, indexing, groove machining and unloading are shown in one cycle.

Film · 02 · 0:11

SDS Drill Bit Spiral-Flute Machining

Close-up factory footage of the helical flute being machined into a large SDS drill body.

Visible record — The cutting action, formed flute and removed steel chips are visible.

Film · 03 · 1:02

Automated SDS Drill Bit Flute Machining

A close view of automated spiral-flute machining on an SDS drill body.

Visible record — Repeated positioning, clamping and spiral-flute machining are shown in close detail; SDS shank-groove production is covered in the dedicated shank-machining record.

Film · 04 · 1:09

Automated SDS Shank Machining

A second enclosed station processes fluted SDS drill bodies at the connection end.

Visible record — Fluted drill bodies, repeated clamping and the enclosed machining cycle are shown; no dimensional tolerance is claimed.

§ II · Heat Treatment

Salt-Bath and Controlled-Atmosphere Heat Treatment.

Zhonghuan supports two controlled routes for SDS steel bodies. Isothermal salt-bath treatment uses full-surface molten-salt contact for rapid, uniform heat transfer and a controlled hold. Controlled-atmosphere heat treatment uses an enclosed furnace recipe to manage the thermal curve and limit oxidation or decarburization exposure. The route is selected by steel grade, geometry and approved program.

HT · 01

Route, alloy & section matched

Salt-bath or controlled-atmosphere treatment is selected against the approved SDS body steel, diameter and impact duty rather than copied across every SKU.

HT · 02

Bath / atmosphere control

Bath temperature and hold, or furnace zones and protective atmosphere, are controlled with transfer time and load density to limit gradients, oxidation and distortion.

HT · 03

Release by evidence

Release is based on the approved cycle record, hardness by inspection zone, straightness/runout after cooling and the project sample plan. Temperatures, salt chemistry or furnace atmosphere, zone times and holds remain tied to the approved alloy and geometry.

§ III · Brazing 02 / 07 Records

Two Routes to the Carbide Joint.

Zhonghuan uses two current brazing routes for carbide-insert drill bits. The premium continuous controlled-atmosphere mesh-belt furnace supports stable volume production with the cleanest, most uniform joint appearance; nitrogen-shielded high-frequency induction brazing supports selected standard professional programs with a flexible production cycle. Full-carbide-head programs are presented separately under the RFW construction.

Film · 05 · 0:58

Nitrogen-Shielded High-Frequency Induction Brazing of an SDS Carbide Tip

The carbide-head joint is heated by high-frequency induction while nitrogen shields the brazing area from the surrounding atmosphere.

Visible record — The induction coil, controlled heating cycle and glowing joint area are visible.

Continuous Controlled-Atmosphere Mesh-Belt Brazing Furnace Still · 06

Continuous Controlled-Atmosphere Mesh-Belt Brazing Furnace

A continuous mesh-belt furnace carries assembled carbide-tipped drill bodies through controlled preheat, brazing and cooling zones under a protective atmosphere for repeatable volume production.

Visible record — The mesh-belt feed, enclosed multi-zone furnace and independent temperature controls are visible.

§ IV · Straightening 01 / 07 Record
Film · 07 · 0:30

Straightness Is Corrected, Not Assumed.

Correction Cycle

The final record shows automated loading, rotary holding and a controlled correction cycle—the finishing sequence used to bring drill-body straightness into the project inspection workflow.

Automated SDS Drill Bit Straightening

Visible record — Automated loading, rotary holding and the straightening cycle are shown; no numerical runout tolerance is claimed.

§ V · Reading the Record

A visible production chain, built for repeatable SDS manufacturing.

From forming and isothermal salt-bath heat treatment to brazing and straightening, this archive shows the equipment, workflow and process discipline behind Zhonghuan SDS production. For OEM programs, cycle evidence, joint requirements and inspection scope are aligned with the approved specification.

N·01

What is documented?

The equipment, handling sequence and visible material transformation in each specific shot.
N·02

What can be specified?

Groove geometry, dimensional tolerance, joint requirements and inspection scope can be aligned to the approved OEM specification.
N·03

How is application fit evaluated?

Review real drilling footage in the Test Lab, then request samples matched to your substrate, hammer, diameter and working depth.
Colophon · Contact

Send the SDS specification. We review the manufacturing fit.

OEM / Private Label

Connection type, diameter range, working length, head geometry, packaging and target market are enough to begin.