
What a Real SDS Drill Bit Data Sheet Does
An SDS drill bit technical data sheet should not be a decorative catalogue page. It should answer a procurement question: will this bit drill the right hole, in the right material, with the right machine, for the service life and anchor risk your channel expects?
This guide is deliberately narrow. It covers SDS-Plus, SDS-Max and straight-shank masonry drill bits used to make holes in concrete, brick, block and stone. It does not cover core bits, hollow dust-extraction bits, chisels, adapters or pilot-drill systems.
A useful SDS / masonry drill bit data sheet usually has seven groups of information: drill diameter, working length, total length, head geometry, shank system, material suitability, and quality or certification language. The fields look simple, but they decide whether the bit is a commodity masonry SKU or a professional anchor-hole product.
| Data-sheet field | What it really controls | Buyer risk if missing |
|---|---|---|
| Drill diameter | Actual nominal hole size | Wrong anchor fit or no comparable quote |
| Working length | Usable drilling depth | Under-drilled anchors and false length assumptions |
| Head geometry | Speed, roundness, rebar behavior and service life | Cheap 2-cutter sold as premium reinforced-concrete bit |
| PGM / wear mark | Anchor-hole suitability and retirement point | Users keep drilling after the hole is no longer within anchor assumptions |
| Shank system | Machine compatibility and impact-energy transfer | SDS-Plus, SDS-Max and cylindrical shank confusion |
Diameter, Working Length and Total Length
The diameter line is not only a size label. For anchor drilling it is the first engineering claim. An M10 anchor, a 3/8 inch wedge anchor and a concrete screw are all built around a defined hole diameter. If the bit does not drill that hole accurately, the anchor system is not being installed under the condition used for its published load data.
The data sheet should separate working length from total length. Total length is measured from carbide tip to shank end. Working length is the fluted, usable section that can actually clear dust and reach the required depth. A 160 mm SDS-Plus bit does not drill 160 mm deep. The SDS shank consumes part of that length inside the chuck.
For procurement, ask suppliers to quote both numbers in the same line: diameter x working length x total length. A line such as 10 x 100 x 160 mm is much easier to audit than a vague 10 mm x 160 mm listing.
Head Geometry and Material Fit
Start with the substrate, reinforcement conditions, hammer platform and required hole. Then read cutting-edge geometry, carbide-component count and joining method as separate fields. The five illustrated examples below show how the same cutter count can describe different constructions.
| Material / job | Data-sheet wording to expect | Practical bit choice |
|---|---|---|
| Brick, block, light masonry | Concrete, brick, block, masonry | 2-cutter SDS-Plus or masonry bit |
| Plain concrete | Concrete, general construction | 2-cutter or 4-cutter depending on duty level |
| Reinforced concrete | Reinforcement chamfer, 4-cutter, full carbide head, rebar-tolerant | 4-cutter or full-carbide-head SDS bit |
| Anchor holes | PGM, wear mark, hole accuracy, round holes | PGM-oriented 4-cutter or tested professional line |
| Hard stone / granite-like aggregate | Hard stone, natural stone, tough carbide grade | Premium carbide and stable head geometry |
Five Illustrated Head Examples: Read the Construction Behind the Name
Cutting edges, carbide pieces and joining method answer three different questions. A 3-cutter can also be a full carbide head; a compact four-cutter can also use several inserts. Our examples show the fields a useful technical sheet should separate, rather than treating these catalogue names as a universal quality ladder.
| Catalogue example | Active cutting edges | Carbide components in this example | Head-to-steel joining |
|---|---|---|---|
| 2-cutter brazed insert | 2 | 1 carbide plate | Brazing |
| 3-cutter full carbide head | 3 | 1 three-edge carbide head | Resistance friction welding in our programme |
| Compact brazed 4-cutter | 4 | Primary blade plus compact side inserts; confirm the supplied layout | Brazing |
| ZHMAX-7 multi-insert 4-cutter | 4 | 3: one primary blade and two side inserts | Brazing |
| 4-cutter full carbide head | 4 | 1 four-edge carbide head | Resistance friction welding in our programme |
1. Two-Cutter: One Carbide Plate, Two Main Edges
Our two-cutter examples show a full-width carbide plate and the steel body that carries it. Standard and raised-centering profiles share two main cutting edges. For concrete, brick and block work, a useful sheet identifies the tip profile, finished cutting diameter, body and intended SDS hammer.
The insert drawing adds another useful distinction: its D, W and T fields describe carbide geometry. Working length and overall length describe the finished drill bit. Read the angles against that specific insert drawing.
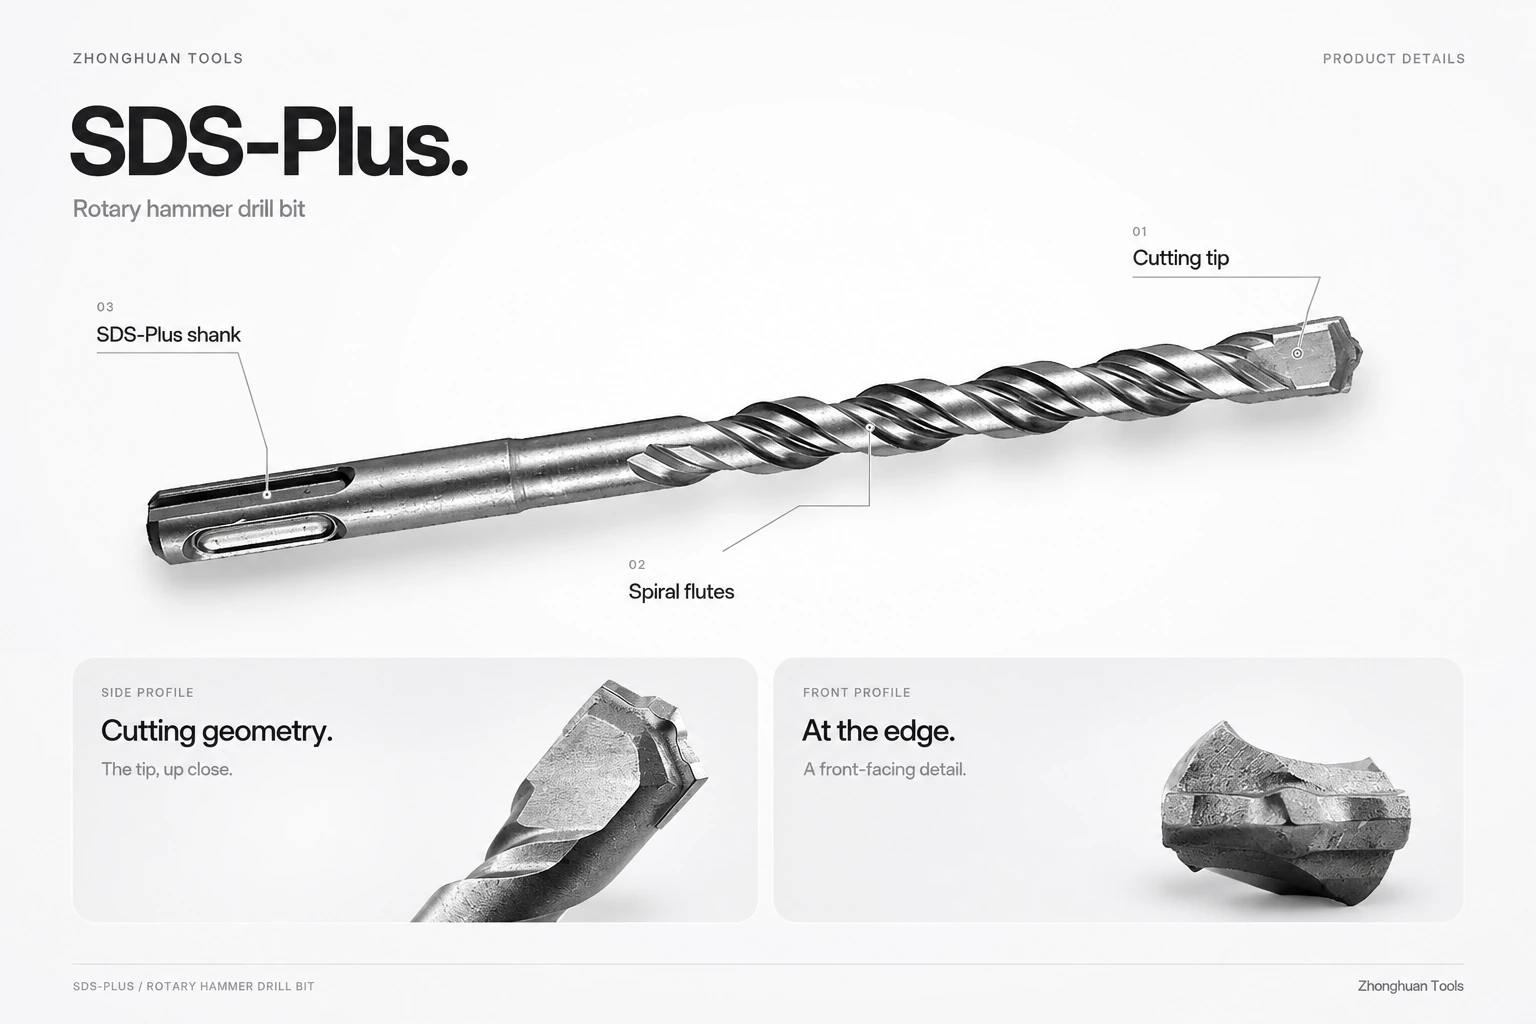
Two-cutter SDS-Plus: assembled bit and tip views.
View full-size image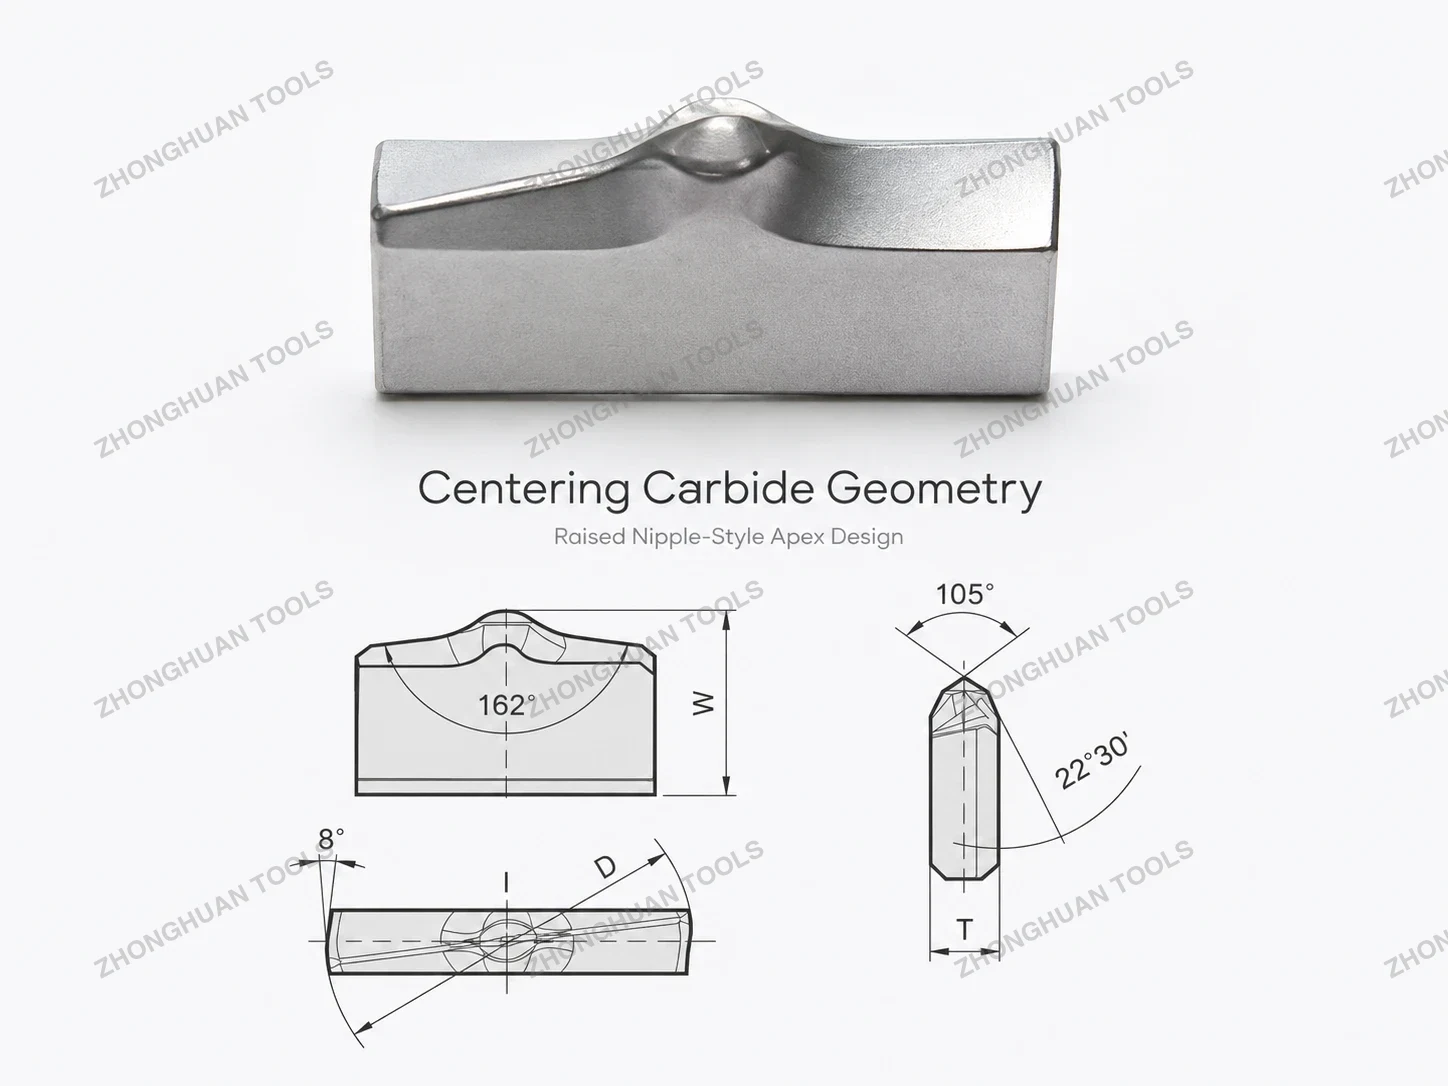
Raised-centering insert: component dimensions and grinding geometry.
View full-size imageExample data-sheet entry: 2 cutting edges / 1 carbide plate / brazed insert / SDS-Plus; add the selected centering profile and the SKU’s diameter × working length × overall length.
2. Three-Cutter: Record the Three Edges and the Joint
The illustrated Y head has three cutting directions spaced at 120° around the centre. Our SDS-Plus three-cutter full-head programme forms those edges in one carbide component joined to the steel body by resistance friction welding. Here, “3-cutter” describes the working geometry and “full carbide head” describes the construction.
On another supplier’s sheet, the same three-cutter label may accompany an inserted and brazed tip. Ask the sheet to name the joint and show the flute entrance and head-to-body connection. The edge count alone is not a joint specification.
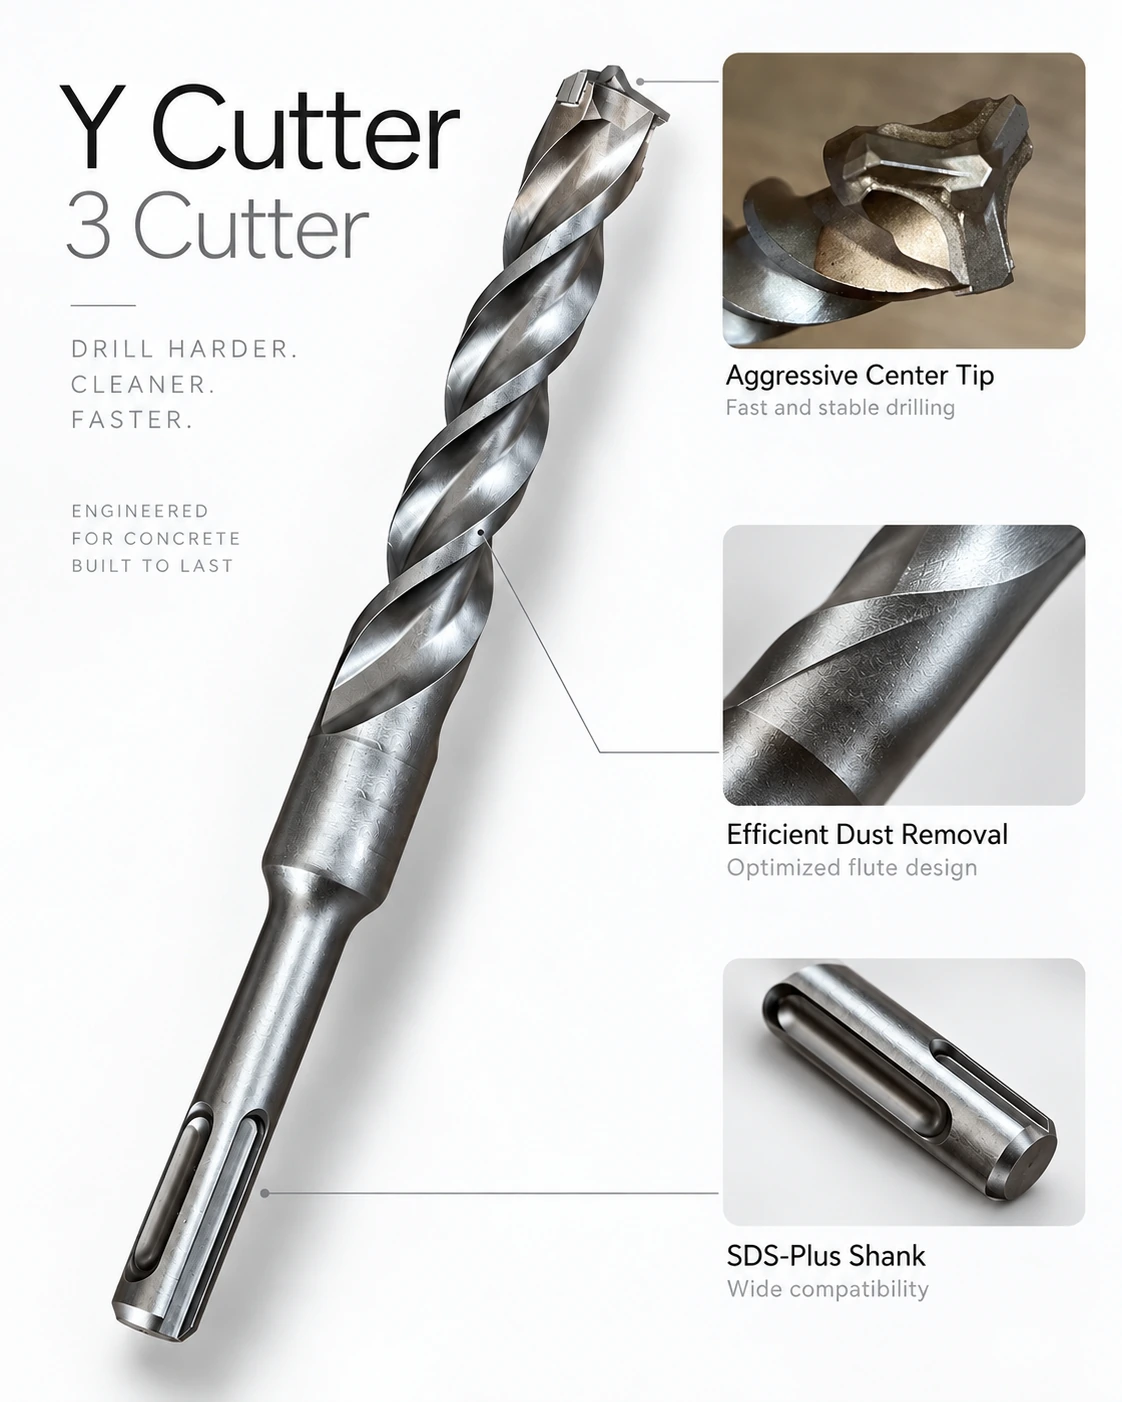
Three-edge Y head: head geometry and SDS-Plus body.
View full-size image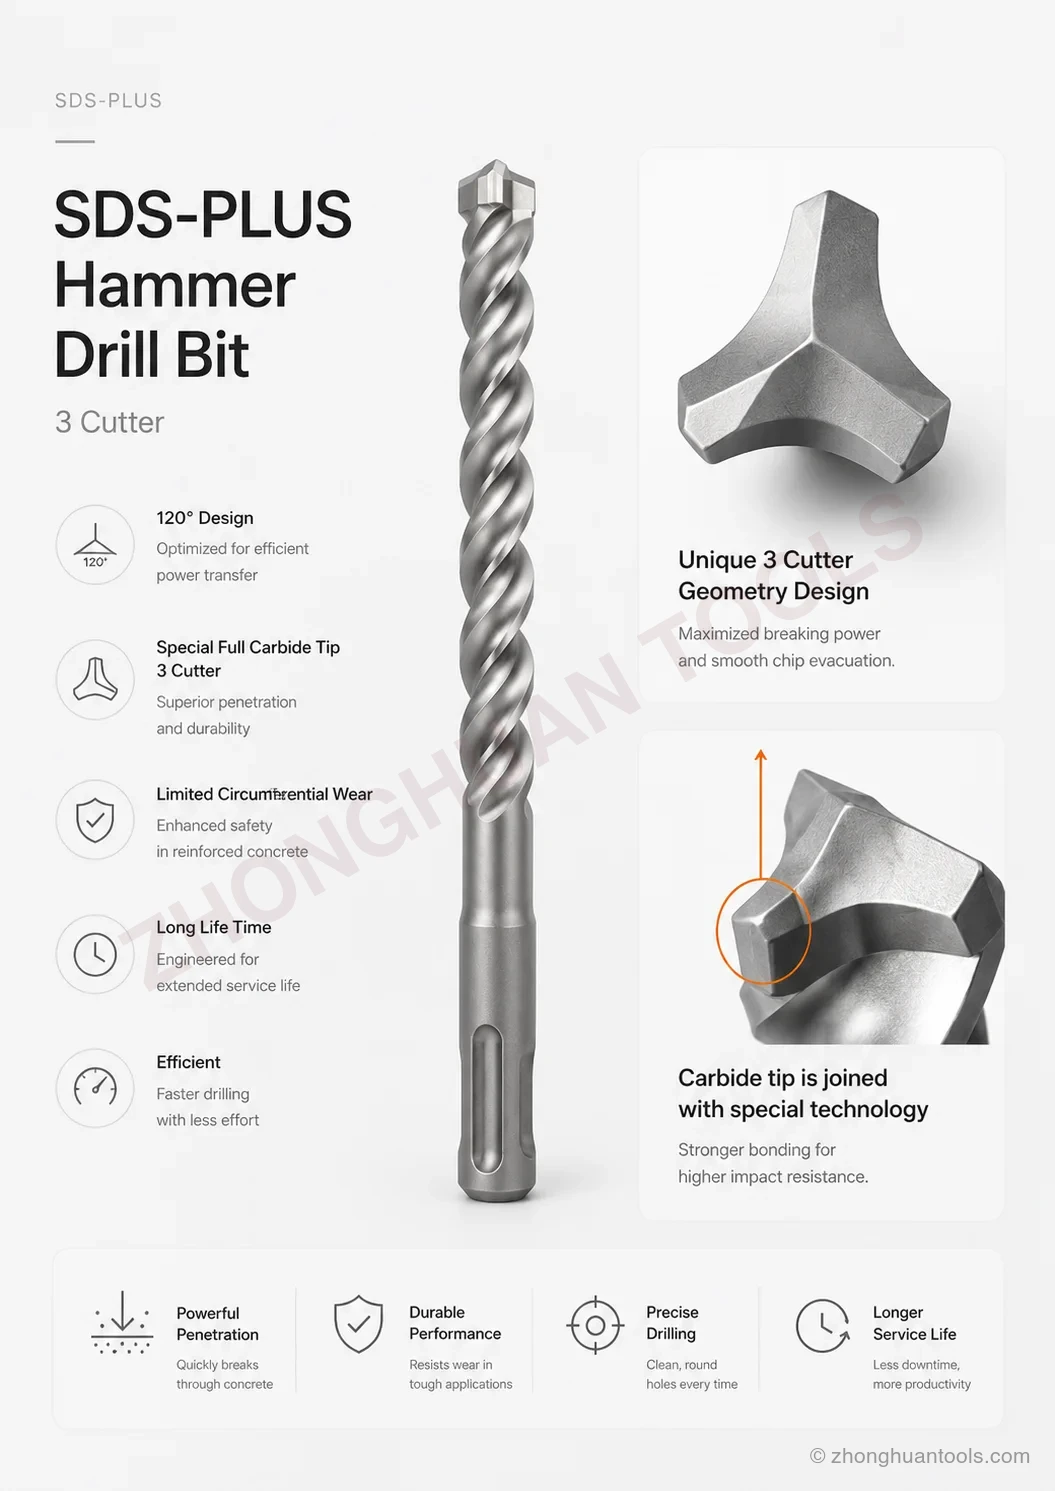
Three-cutter full head: carbide component and head-to-body connection.
View full-size imageExample data-sheet entry: 3 cutting edges / one-piece carbide head / resistance friction-welded joint / SDS-Plus; record the three-edge geometry and finished dimensions separately.
3. Conventional Four-Cutter: A Compact Brazed Cross
The 5X close-ups show a compact cross arrangement with four active edges supported by the steel head. This is a useful example of the conventional brazed four-cutter description buyers encounter in catalogues. Check the primary blade, side inserts, steel seats and clearance into the flutes.
“4-cutter” does not mean four separate carbide pieces. A primary blade and two side inserts can produce four edges, as in the multi-insert family. The supplied drawing must fix the component layout; compare diameter, head symmetry and hole-gauge retention under the intended concrete and hammer conditions.
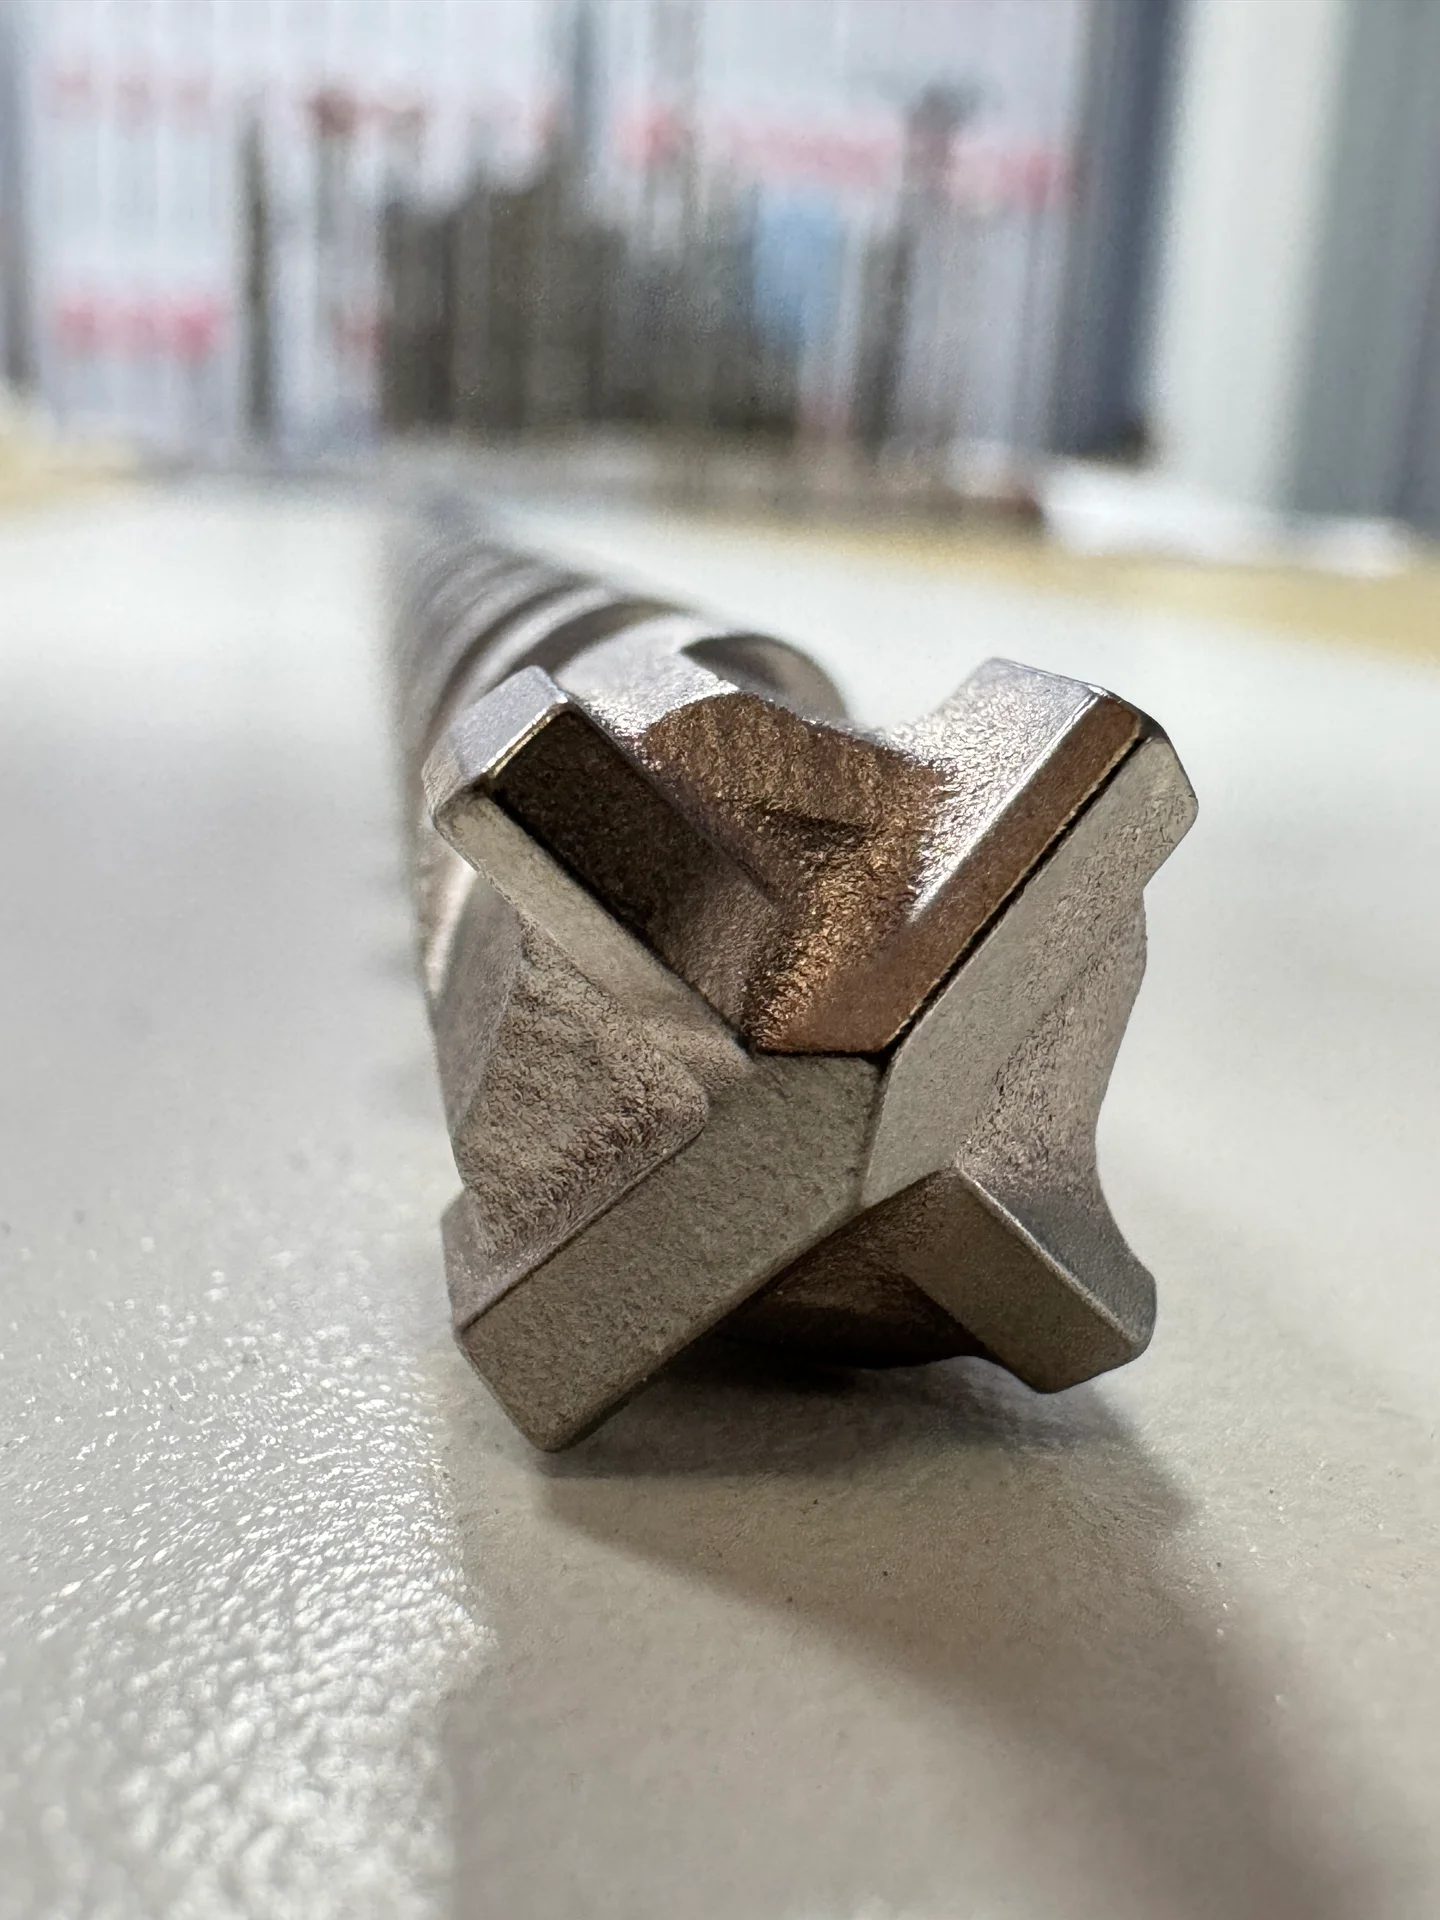
Compact four-cutter: factory head close-up.
View full-size image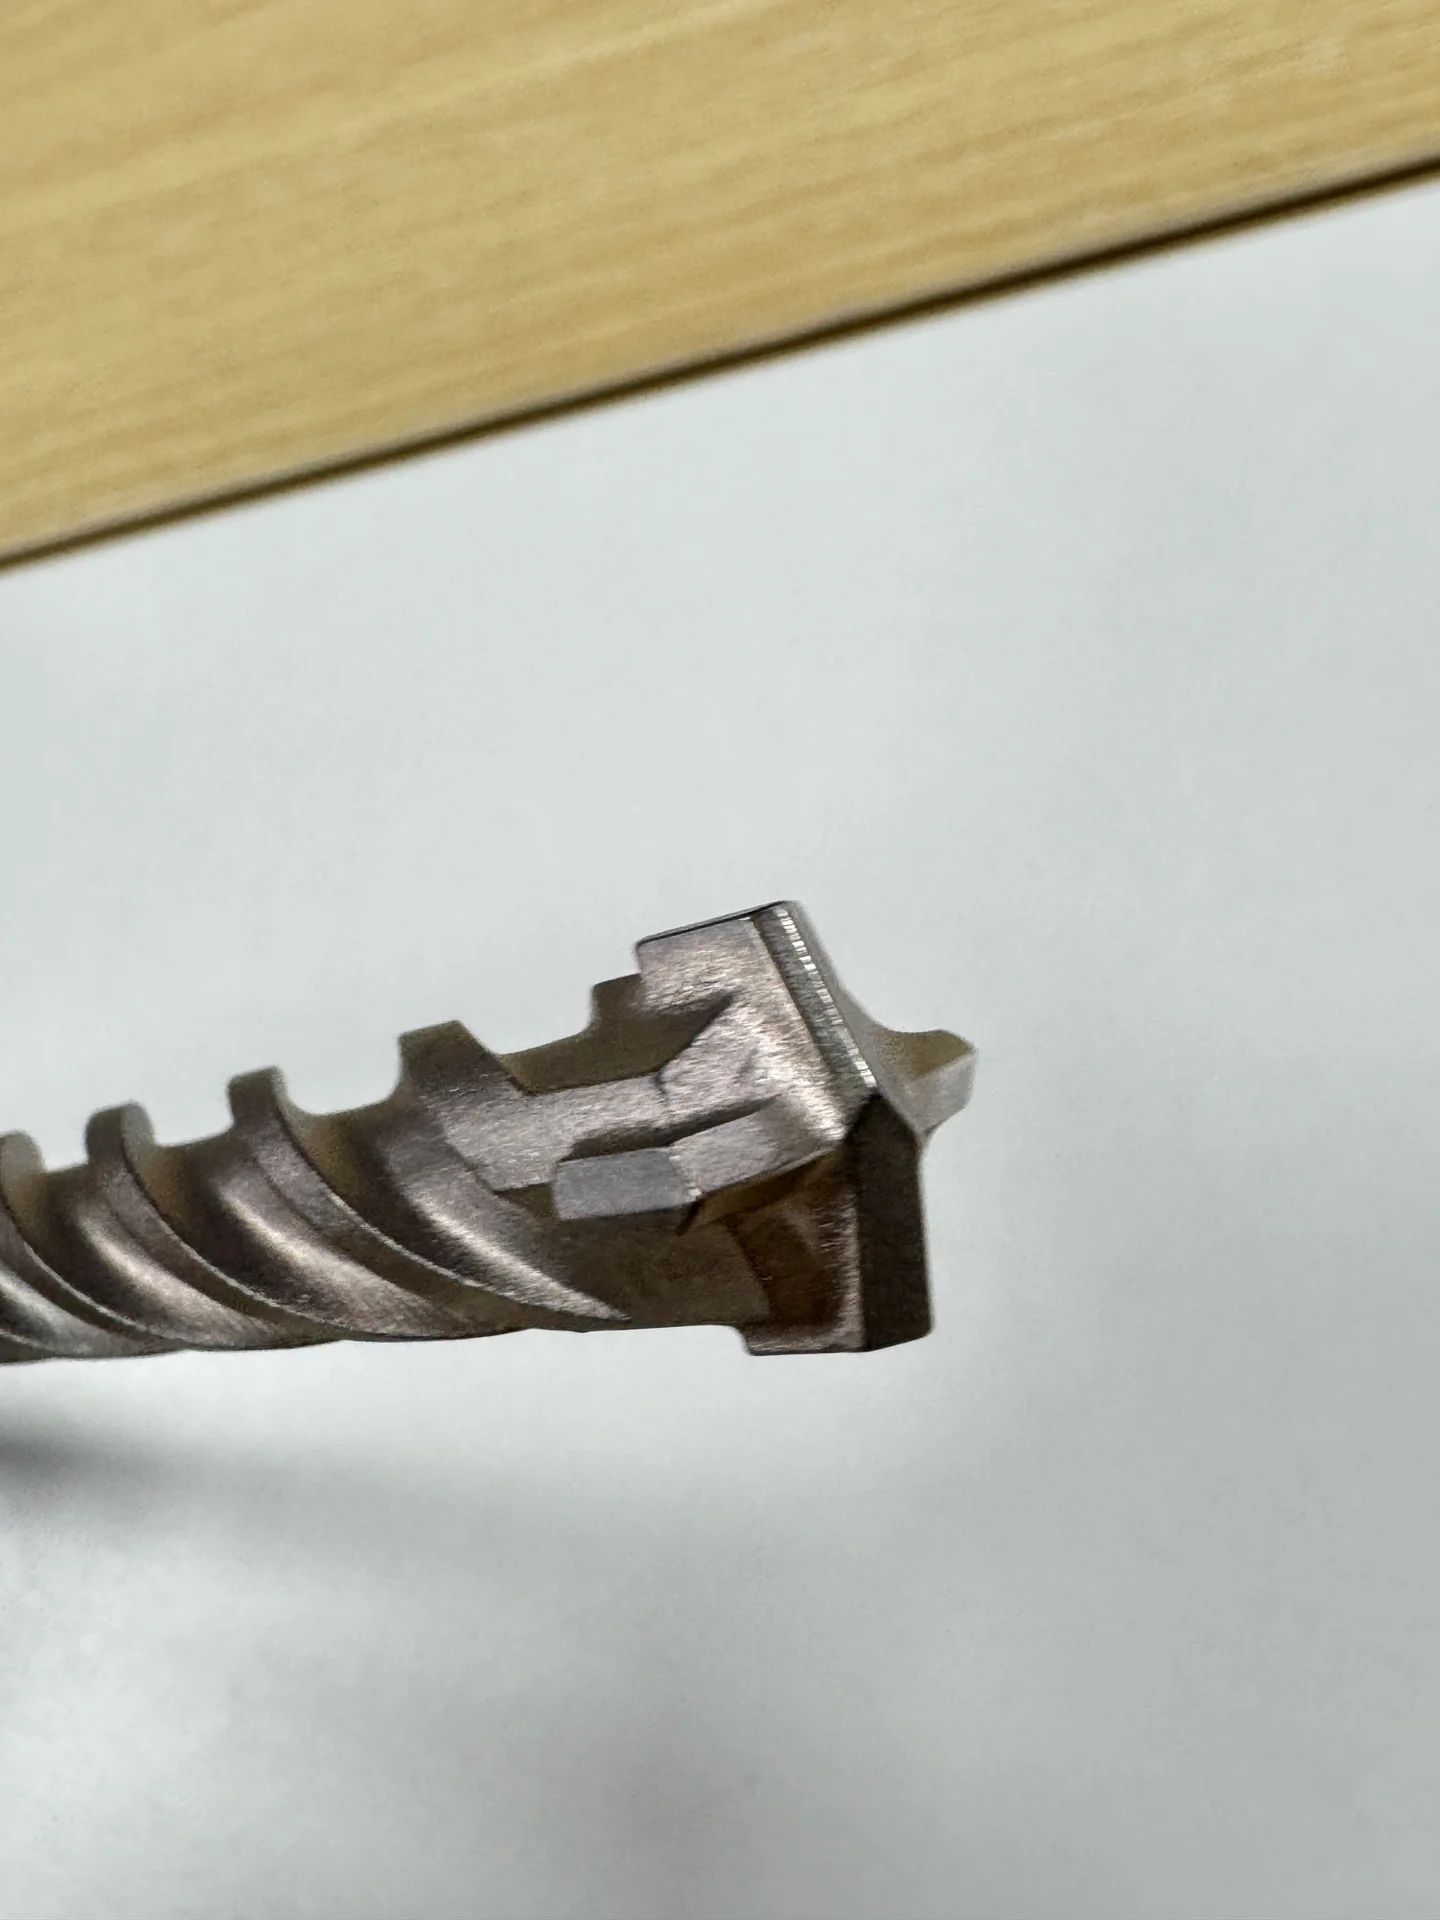
Side view: carbide support, steel seats and flute entrance.
View full-size imageExample data-sheet entry: 4 cutting edges / compact brazed cross / primary-blade and side-insert layout per drawing / SDS-Plus or SDS-Max as explicitly listed.
4. Multi-Insert Four-Cutter: ZHMAX-7 Primary and Side Blades
ZHMAX-7 makes the component count explicit: one full-width primary carbide blade plus two inclined, axially set-back side inserts. The primary blade forms two leading edges; each side insert contributes one peripheral edge. Three carbide pieces therefore provide four active cutting edges.
A compact cross and ZHMAX-7 can share that component count. The useful comparison is the blade profile, side-insert inclination and axial position, steel support and flute entry. For this SDS-Max programme, ask the technical sheet to show the assembled head and loose-component drawing together.
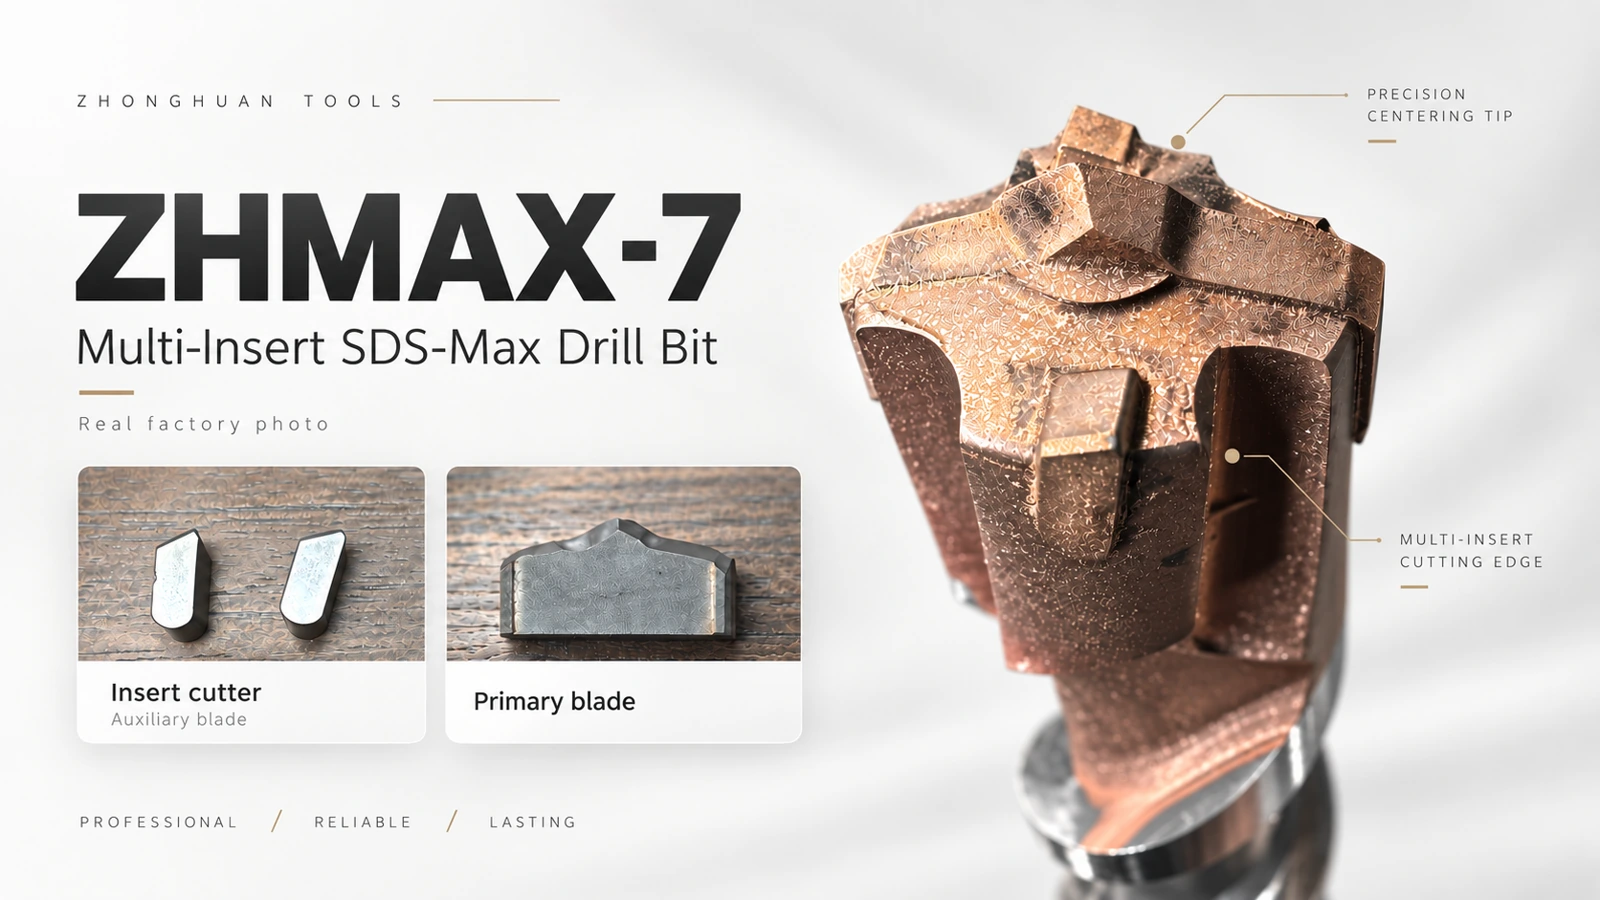
ZHMAX-7: assembled head and the three carbide components.
View full-size image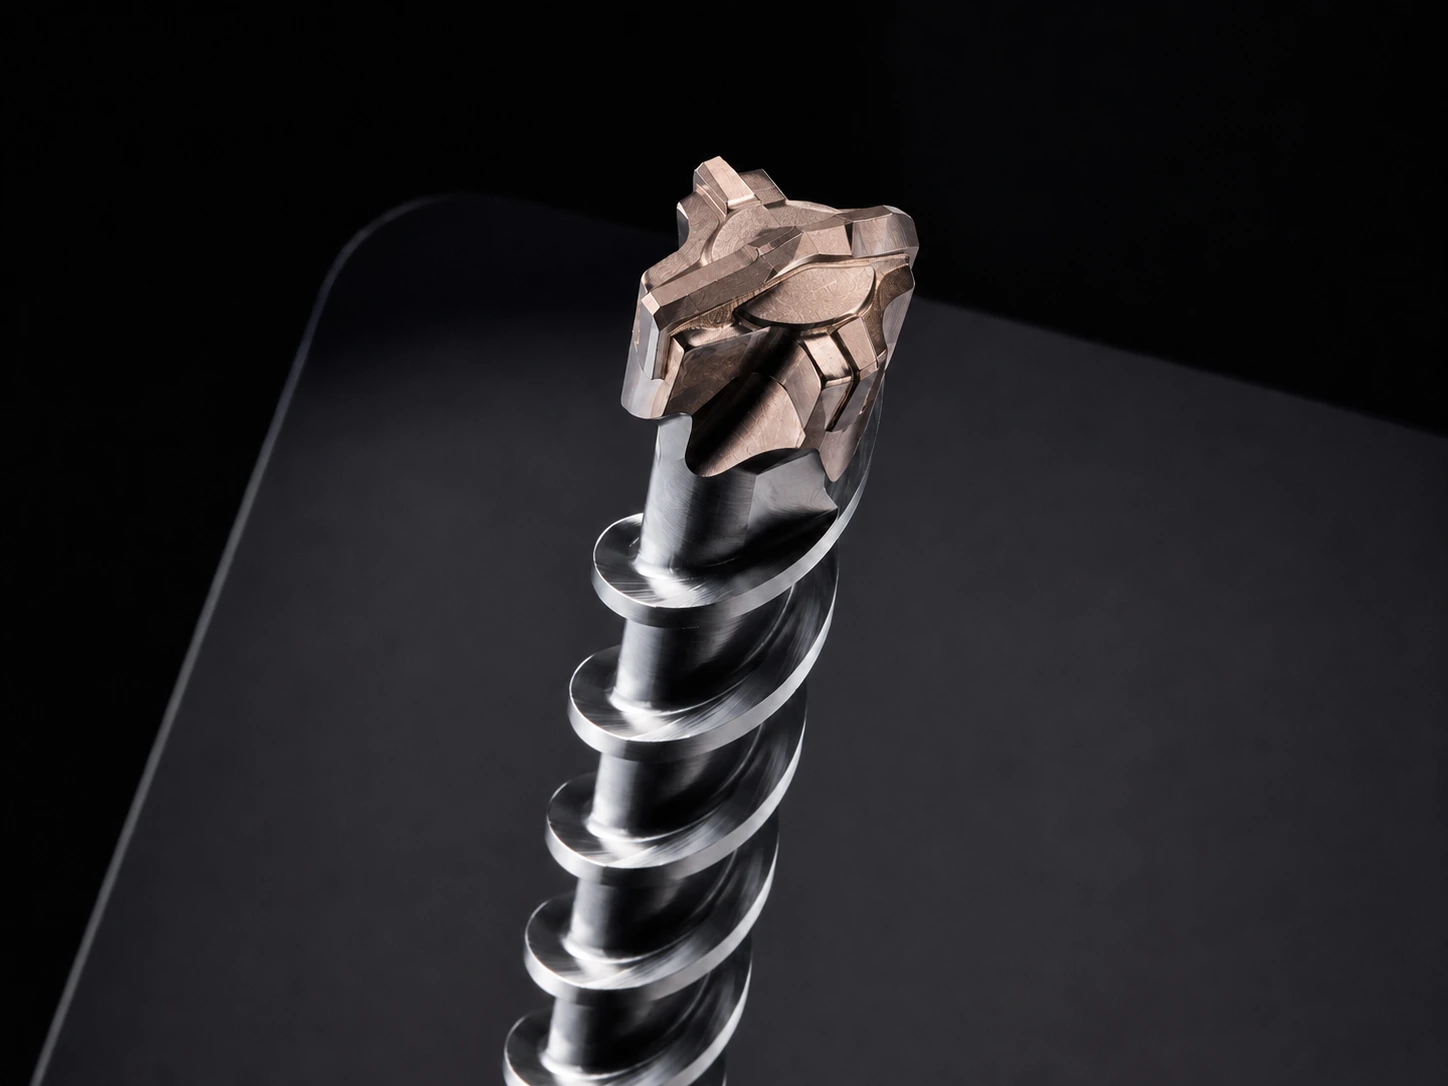
ZHMAX-7 close-up: primary blade, side inserts and steel support.
View full-size imageExample data-sheet entry: 4 cutting edges / 3 carbide components / full-width primary blade plus two inclined, axially set-back side inserts / brazed assembly / SDS-Max.
5. Four-Cutter Full Carbide Head: One Working Head, Four Edges
Our ZHPLUS-8 and ZHMAX-8 examples use one carbide working head with four cutting edges, joined to a steel body through resistance friction welding. The head is carbide; the spiral body and shank remain steel. The one-piece head still has a head-to-steel connection that belongs on the technical sheet.
Read the edge count, full-head geometry, joint, wear criterion and machine interface separately. The images include SDS-Max head detail and an SDS-Plus complete-bit view: a shared head-construction family does not make the two shanks interchangeable.
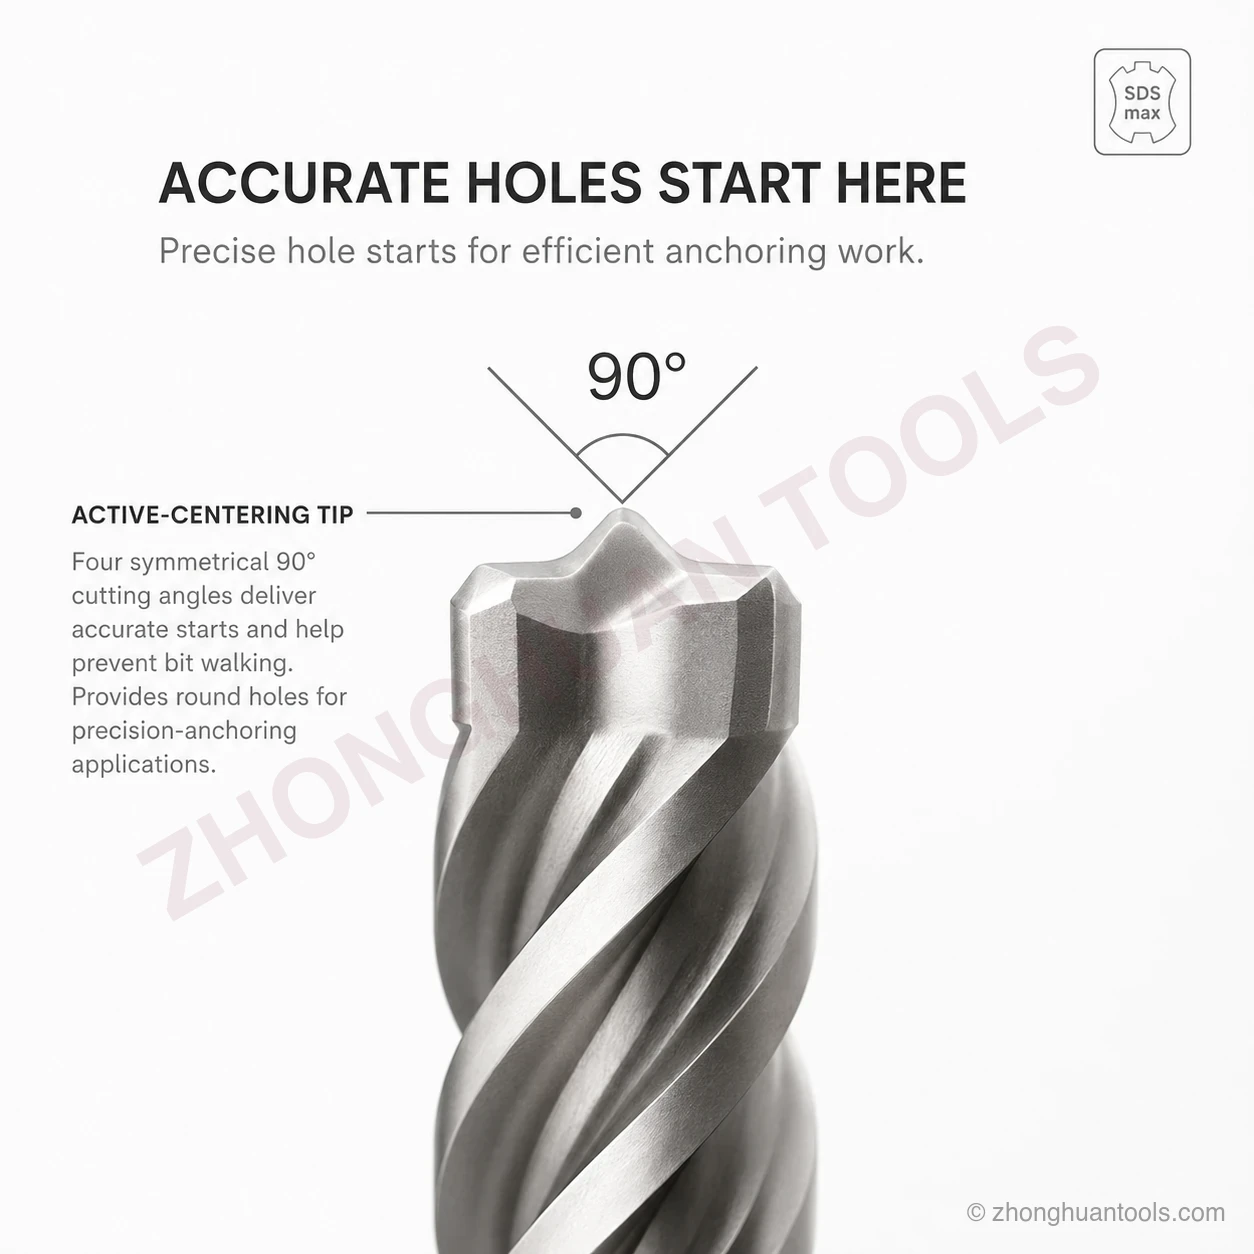
ZHMAX-8 SDS-Max: one-piece four-edge carbide head.
View full-size image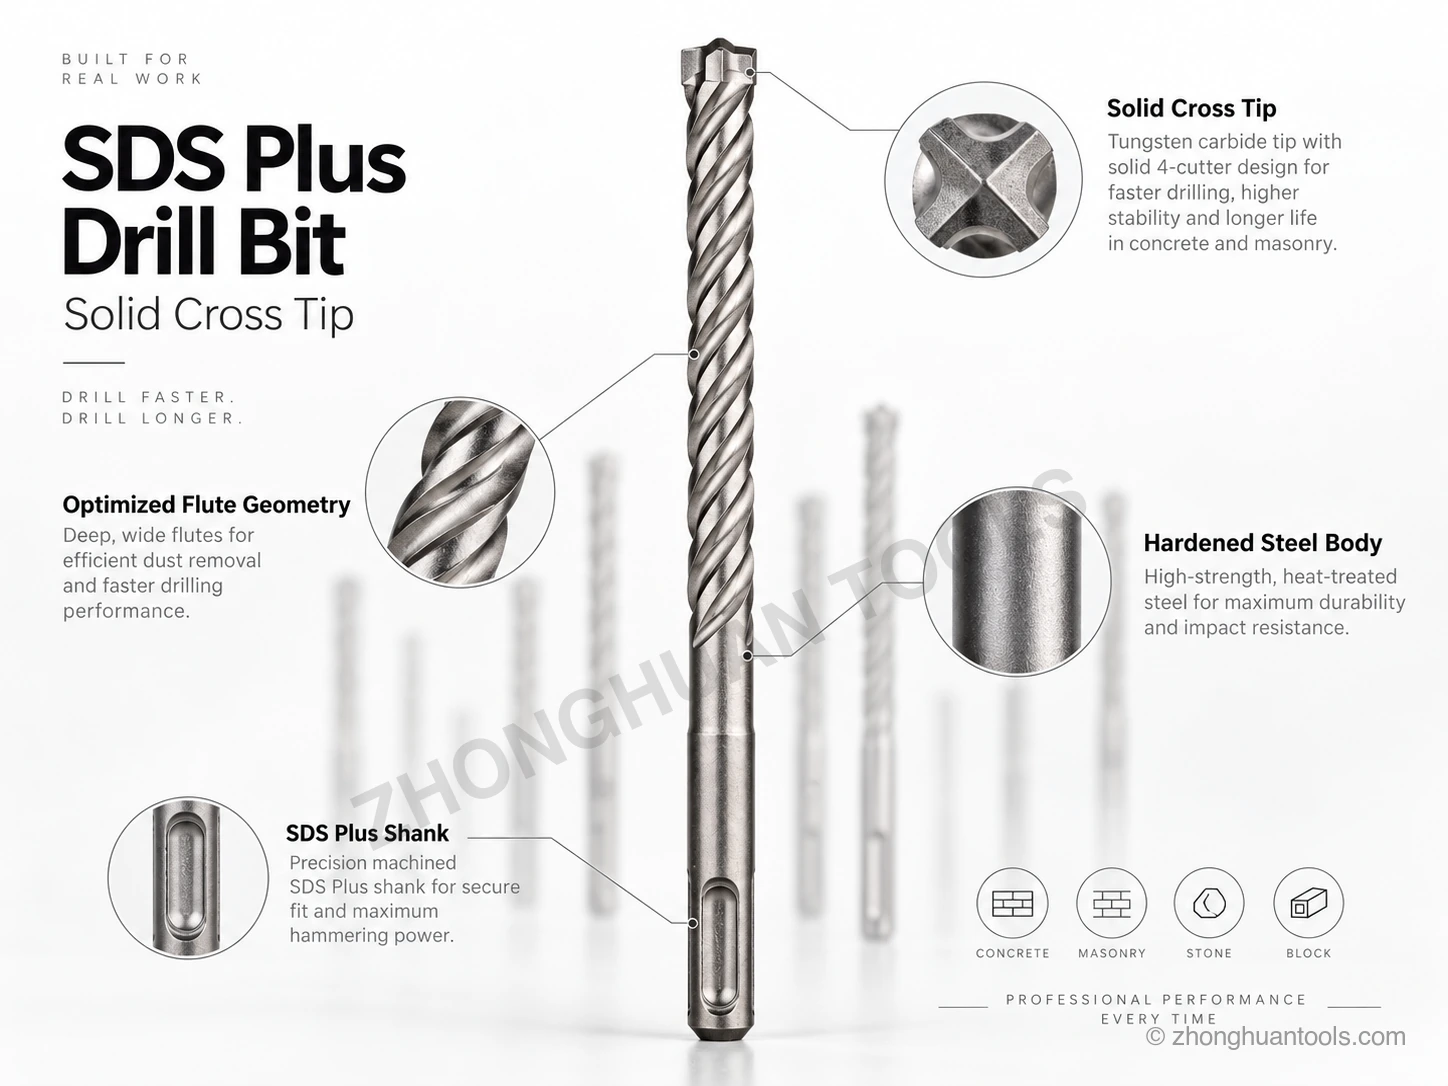
ZHPLUS-8 SDS-Plus: full head, steel body, flutes and shank.
View full-size imageExample data-sheet entry: 4 cutting edges / one-piece full carbide head / resistance friction-welded head-to-steel joint / specified SDS-Plus or SDS-Max interface and approved size matrix.
For a comparable quotation, keep the construction line separate from the size line. A format such as 10 × 100 × 160 mm identifies diameter × working length × overall length only when the sheet names that order. Pair it with the chosen head construction, substrate and hammer. We confirm the finished dimensions, carbide drawing and joining route for each OEM SKU.
PGM and Wear Mark
The wear mark is the field most buyers overlook. It is not a marketing stripe. It is a user-visible retirement indicator. When the outer carbide cutting edges have worn to the wear mark, the bit should no longer be used for anchor-hole work because the drilled hole may no longer stay inside the diameter and shape assumptions used for certified anchor installation.
Why does that matter? The hole is the hidden part of the anchor system. A wedge anchor, sleeve anchor, drop-in anchor or bonded anchor only performs as rated when the hole diameter, roundness, depth, cleaning condition and substrate match the tested condition. A bit can still spin and make dust after the wear mark is reached, but that does not mean it is still making an anchor-grade hole.
Official PGM guidance is useful here. PGM states that standard masonry and hammer drill bits are checked for cutting-plate diameter, cutting-plate height, symmetry and eccentricity of the cutting plate, and drill-bit runout. PGM also explains that drill bits within these tolerances are used for ETA anchor pull-out tests, which is why PGM-marked bits are relevant to safe anchor installation with ETA and CE-marked anchors. For multicutter hammer bits, PGM requires comparison pull-out tests showing that anchor pull-out forces in multicutter holes are equal to those in standard-drill-bit holes.
That is the practical meaning of PGM language on a data sheet: it is not just a badge on the package. It is a claim about the hole the bit can produce while the bit remains within its usable wear state.
Hole Diameter and Anchor Capacity
Wear affects anchors through hole geometry. A worn carbide head usually loses outside cutting diameter first. That can create an undersize hole, especially at the start of the hole. Asymmetric wear, poor brazing, runout or a bent body can also create an out-of-round or oversize hole along one axis. Both failure modes are bad for anchors.
In past Zhonghuan Tools internal durability checks, repeated drilling showed a consistent direction: once the carbide outside diameter starts to wear, drilling speed slows, rebar contact becomes more damaging, and hole diameter and roundness become less stable. We use that observation as the practical link between wear-mark discipline and anchor-hole reliability.
| Hole condition | What can happen | Anchor risk |
|---|---|---|
| Undersize hole | Anchor is forced in, insertion depth may be wrong, torque feels high because of wall friction | False installation torque, damaged sleeve or incomplete seating |
| Oversize hole | Expansion pressure drops or bonded-anchor annular gap becomes untested | Lower pull-out resistance and invalid comparison with published load tables |
| Out-of-round hole | Anchor contacts on high spots and gaps remain elsewhere | Uneven expansion, resin voids or unpredictable load transfer |
| Too shallow | Working length was misread or dust remained at the bottom | Reduced embedment and failed pull-out test |
This is why a wear mark belongs on a professional SDS data sheet. It gives the user a simple field rule: keep the bit for general non-critical masonry work if appropriate, but retire it from anchor-hole service once the wear limit is reached. For structural anchor work, the conservative rule is to retire on gauge, not on breakage.
Shank System and Machine Class
A data sheet should state SDS-Plus, SDS-Max or cylindrical shank clearly. SDS-Plus and SDS-Max are not quality grades; they are machine interfaces. SDS-Plus uses the smaller rotary-hammer class for most construction anchor holes. SDS-Max is for larger diameter, deeper or heavier impact work.
Recommended speed is less useful for SDS hammer bits than it is for HSS twist drills or diamond blades. A better SDS data sheet states the intended hammer class, diameter range and duty level. If a bit is large but the user runs it in an underpowered SDS-Plus hammer, drilling slows, heat rises and carbide wear accelerates. That is a machine match problem, not only a bit quality problem.
Data-Sheet Red Flags
- Only total length is listed. Without working length, users may overestimate usable depth.
- Only material icons are shown. Icons without head geometry, carbide grade or application notes are weak evidence.
- PGM is used vaguely. Ask whether the actual SKU or family is PGM-certified and how it is marked.
- ISO 5468 is written beside SDS shank geometry. ISO 5468 belongs to cylindrical-shank masonry-bit dimensions, not SDS-Plus or SDS-Max groove geometry.
- Wear mark is shown but not explained. The sheet should say it indicates the wear limit for anchor-hole suitability.
- 2-cutter and 4-cutter lines are mixed under one premium claim. Quote them separately.
RFQ Checklist
For a professional SDS drill bit RFQ, write the spec in engineering fields instead of asking for a catalogue copy.
- Shank system: SDS-Plus, SDS-Max or cylindrical masonry shank.
- Diameter x working length x total length for every SKU.
- Head geometry: 2-cutter, 4-cutter, 3-cutter, multi-segment or full carbide head.
- Target materials: brick, block, plain concrete, reinforced concrete, hard stone or anchor holes.
- PGM requirement: required, optional, or not needed for the channel.
- Wear mark requirement: required for anchor-oriented professional ranges.
- Quality checks: head diameter, runout, carbide symmetry, shank fit, brazing or weld integrity, sample drilling test.
- Packaging: single clip, plastic tube, pouch, bulk pack, retail set or private-label case.
Related Procurement Programs
If you are sourcing SDS or masonry drill bits for a distributor, importer or private-label channel, these pages cover the commercial side after the technical sheet is understood.
- SDS Drill Bits Manufacturer & Wholesale Supply - SDS-Plus and SDS-Max OEM supply with head geometry, packaging and batch inspection options.
- PGM-Certified Masonry Drill Bits Manufacturer - PGM-focused buyer guide for anchor-hole ranges and European professional channels.
- SDS-Plus Drill Bits for Anchor Bolt Installation - Precision SDS-Plus bits for mechanical and chemical anchor holes.


